Rubber compounds play an indispensable role in modern automotive architectures, serving as mission-critical barriers for fluid containment, environmental sealing, acoustic dampening, and vibration isolation. From under-hood coolant lines and powertrain mounts to body weatherstripping and high-voltage battery enclosures, formulation choices directly govern vehicle durability, driver comfort, and regulatory compliance. A sub-optimal compound operating within severe automotive duty cycles risks premature hardening, cracking, chemical extraction, or compression failure—leading to costly warranty claims and potential field recalls.
For automotive design engineers and rubber compounders, material development presents an ongoing engineering compromise. Formulators must consistently meet stringent physical performance specifications while controlling raw material costs, maintaining batch-to-batch processability, and complying with ever-stricter global environmental directives.
This comprehensive technical guide details the end-to-end compound development lifecycle—from base polymer selection and filler-plasticizer interactions to cure kinetics, finite element simulation, and production scalability.
Compound development begins by qualifying the base polymer backbone against operational environments, fluid exposure, and OEM engineering specifications (such as SAE J200, ASTM D2000, VDA 675, and GMW3232).
EPDM serves as the workhorse elastomer for exterior weatherstripping, window seals, HVAC ducting, and radiator coolant hoses. Its fully saturated hydrocarbon backbone imparts exceptional resistance to ozone, UV radiation, thermal oxidation, and weathering. In accelerated aging tests, properly formulated EPDM weatherseals exceed 500 hours of ozone exposure without micro-fissuring. EPDM maintains high flexibility across -40°C to +150°C. However, its non-polar structure renders it vulnerable to swelling in petroleum-based oils, fuels, and hydrocarbon greases.
Nitrile butadiene rubber provides outstanding resistance to mineral oils, hydraulic fluids, and fuels due to its polar acrylonitrile (ACN) content. Balancing ACN content (typically 18% to 50%) allows formulators to balance fuel swell resistance against low-temperature glass transition (Tg). For severe duty cycles involving dynamic powertrain sealing, timing belts, and aggressive fuel systems, hydrogenated nitrile (HNBR) removes backbone unsaturation, raising continuous operating thresholds to 150°C while boosting abrasion resistance.
FKM compounds are specified for extreme environments, including crankshaft seals, fuel injector O-rings, and turbocharger interfaces where temperatures exceed 200°C alongside exposure to synthetic lubricants, acidic blow-by gases, and aggressive bio-fuels.
Silicones excel in thermal extremes (-60°C to +200°C) with minimal compression set, making them ideal for automotive lighting gaskets, electronic potting, and turbocharger couplers. Fluorosilicones add solvent resistance for specialized fuel and vapor management applications.
Fillers represent a substantial volume fraction of any technical rubber compound, directly dictating hardness, tensile strength, tear resistance, and dynamic stiffness.
|
Performance Property |
High-Structure Carbon Black (e.g., N330/N550) |
Silane-Coupled Precipitated Silica |
|---|---|---|
|
Initial Storage Modulus |
Higher |
Moderate |
|
Payne Effect (Strain Sensitivity) |
Pronounced |
Significantly Lower |
|
Hysteresis & Heat Build-Up (ASTM D623) |
~2x Higher |
Low / Optimized |
|
Wet Grip / Dynamic Traction |
Moderate |
Superior |
|
Static Dissipation & Conductivity |
Inherently Conductive |
Non-Conductive (Insulative) |
Plasticizers lower compound viscosity, facilitate filler dispersion during internal mixing, lower glass transition temperatures, and improve extrusion flow. In automotive applications, plasticizer selection is constrained by long-term durability and passenger cabin safety standards:
The crosslink density and chemical bond structure govern whether a cured elastomer behaves elastically or suffers permanent plastic deformation under clamp load:
|
Criteria |
Sulfur Vulcanization System |
Organic Peroxide System |
|---|---|---|
|
Crosslink Bond Type |
Mono-, di-, polysulfidic (-Sx-) |
Direct C-C single bonds |
|
Bond Dissociation Energy |
~270 kJ/mol (lower thermal stability) |
~350 kJ/mol (high thermal stability) |
|
Continuous Service Temperature |
Up to 120°C |
Up to 150°C - 175°C |
|
Compression Set (Long-term load) |
Moderate / High (creep susceptible) |
Exceptionally Low (<20%) |
|
Thermal Reversion Resistance |
Prone to reversion at high cure temperatures |
Reversion-free |
|
Tensile & Fatigue Endurance |
Superior dynamic flex life |
Moderate; enhanced via co-agents |
Sulfur vulcanization creates flexible polysulfidic bridges that allow local stress redistribution around micro-defects, making sulfur packages the premier choice for parts subject to continuous dynamic flexure such as suspension dust boots and drive-shaft bellows.
Peroxide crosslinking forms direct carbon-carbon bonds requiring substantially more thermal energy to dissociate. For static engine cooling gaskets, HVAC seals, and turbo hoses subjected to extended clamp retention tests, peroxide cure systems eliminate reversion degradation and deliver minimal compression set. Incorporating polyfunctional co-agents (e.g., TAC, TAIC, or TMPTM) elevates crosslink efficiency and increases modulus.
Electrification transforms performance expectations for traditional automotive rubber components:
Modern automotive formulation demands continuous chemical substance screening from the initial recipe phase:
Automotive Rubber Compound Formulation, Kinetics Modeling, and Physical Testing Workflow
Digital engineering workflows now replace costly trial-and-error physical iterations during compound development:
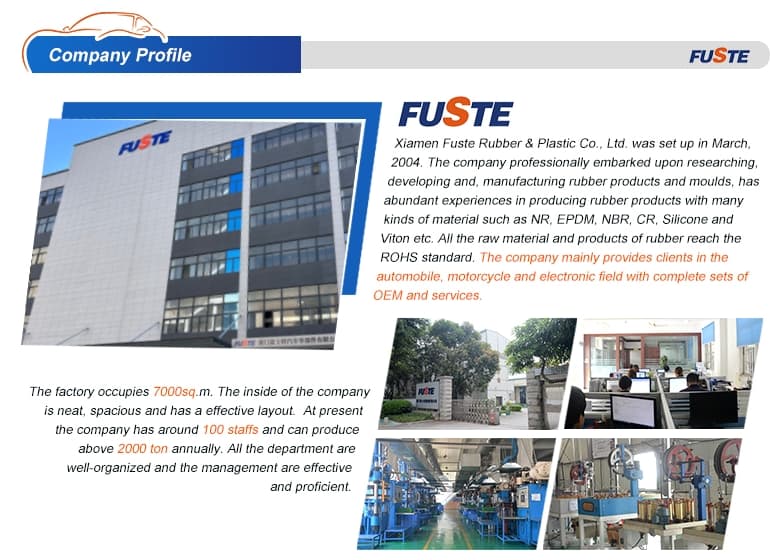
A chemically optimized formulation requires disciplined industrial compounding and precise tool engineering to deliver reliable parts in high-volume production. Fuste Rubber bridges formulation chemistry with scalable automotive manufacturing:
Accelerate Your Development Cycle: Whether you require custom formulation development to meet tight OEM specifications or need to re-engineer an existing component for lower cost and superior life, contact the Fuste Rubber engineering team today to review your technical drawings and compound specifications.
Preventing compression set requires specifying a peroxide-cured EPDM or HNBR polymer system with optimized crosslink density, avoiding high sulfur loadings that degrade above 100°C. Utilizing high-purity paraffinic oils with minimal volatility and maintaining filler loading below 60 phr preserves matrix elasticity under continuous bolted clamp loads.
Blooming occurs when compounding additives (such as insoluble sulfur, primary amine accelerators, or incompatible plasticizing oils) exceed their thermodynamic solubility limit within the cured polymer matrix, migrating to crystallize on the surface. Corrective actions involve balancing accelerator packages, switching to high-solubility plasticizers, or employing secondary retarders to optimize reaction kinetics.
Yes. Thermal expansion coefficients differ significantly between polymer matrices and steel tooling (rubber shrinks roughly 1.5% to 3.5% upon cooling). By integrating cure kinetics, filler loading ratios, and thermal contraction models into virtual CAE packages, tooling engineers can predict differential shrinkage accurately, preventing costly tool rework.
Fuste employs ultra-low volatility, severely hydrotreated paraffinic process oils, and optimized peroxide cure packages that leave minimal volatile reaction byproducts. All materials intended for cabin and under-hood applications undergo rigorous gas chromatography and gravimetric fogging testing in accordance with DIN 75201 standards prior to production release.


 online service


